
Visit our plant without the flight.
Follow a batch through our plant — from the raw material that arrives at the gate to the drum that leaves with its documents. Every step happens in-house.
Six stops. Seven in-house facilities.
Tap a stop to jump to it. Everything on this route is run by our own teams — nothing is outsourced between the raw material and your drum.
- 01 Arrival Microbiological QC · Chemical QC
- 02 Research & development Fermentation R&D lab · API-based R&D lab
- 03 Fermentation Enzyme fermentation unit · Probiotic fermentation unit
- 04 Testing Chemical QC · Microbiological QC
- 05 Quality assurance Quality Assurance
- 06 Packing & dispatch Quality Assurance
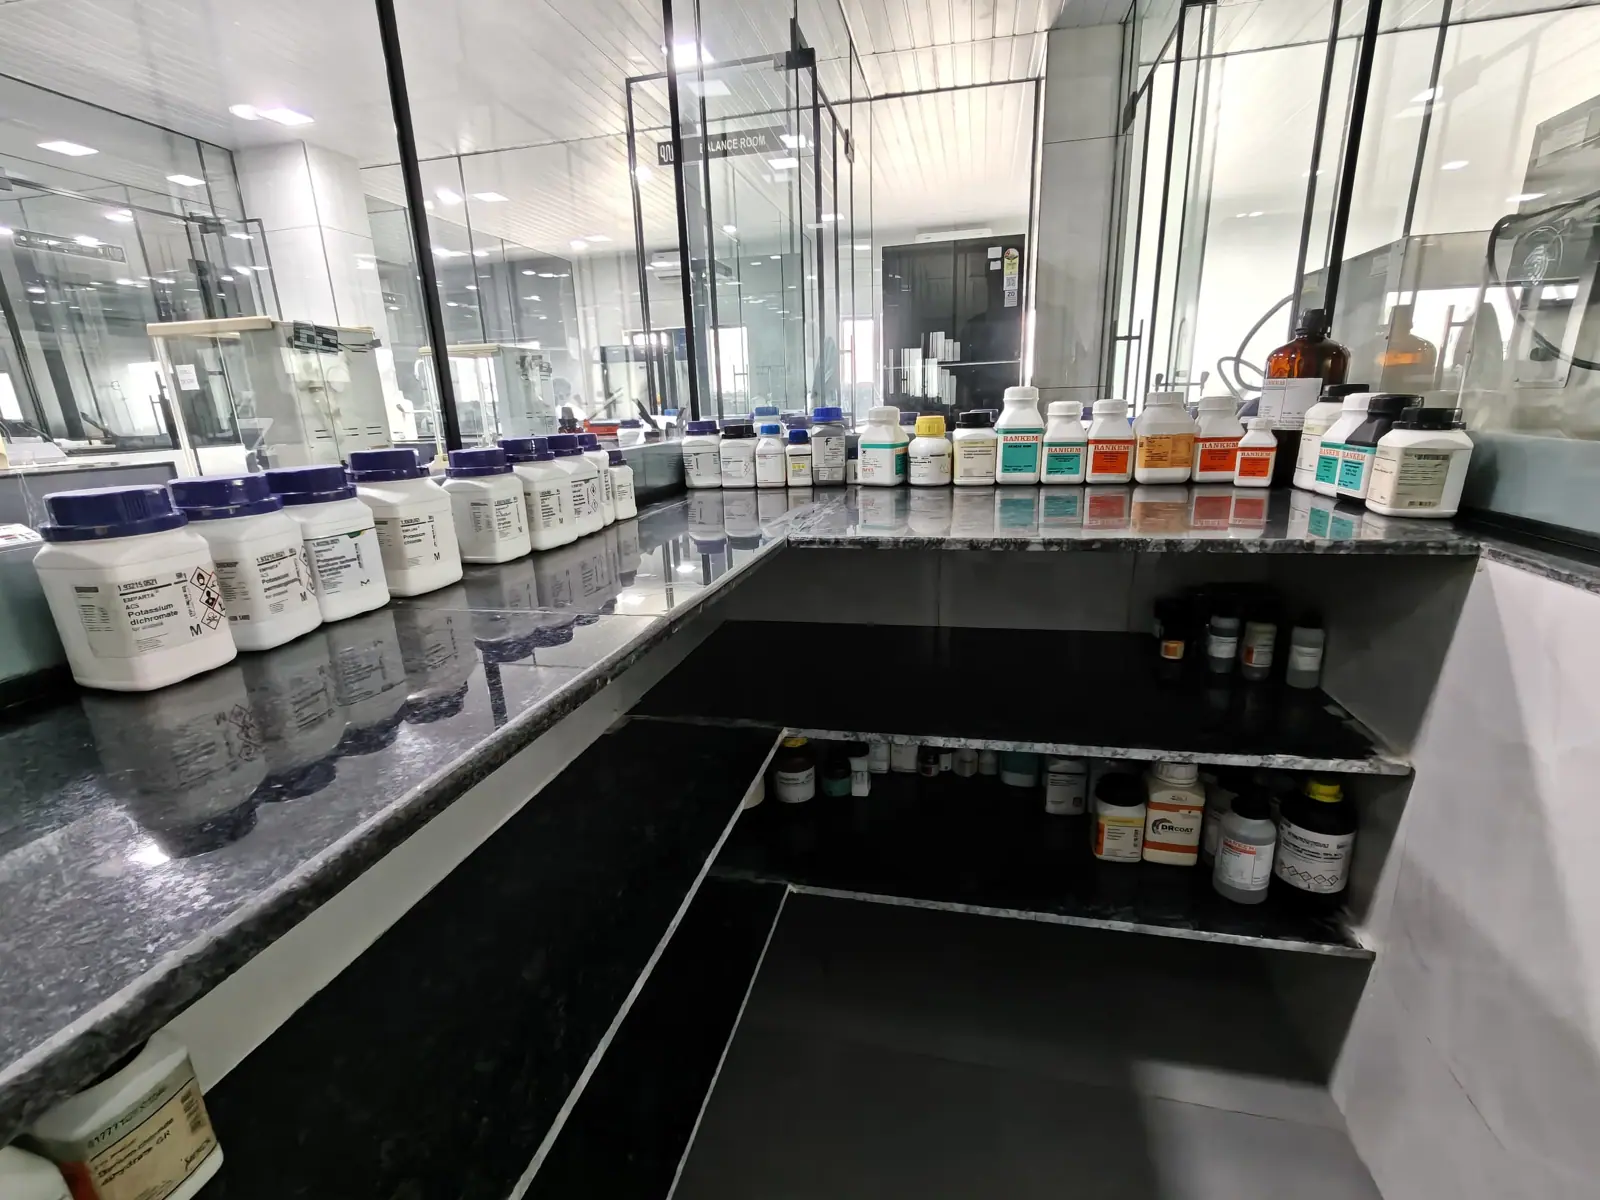
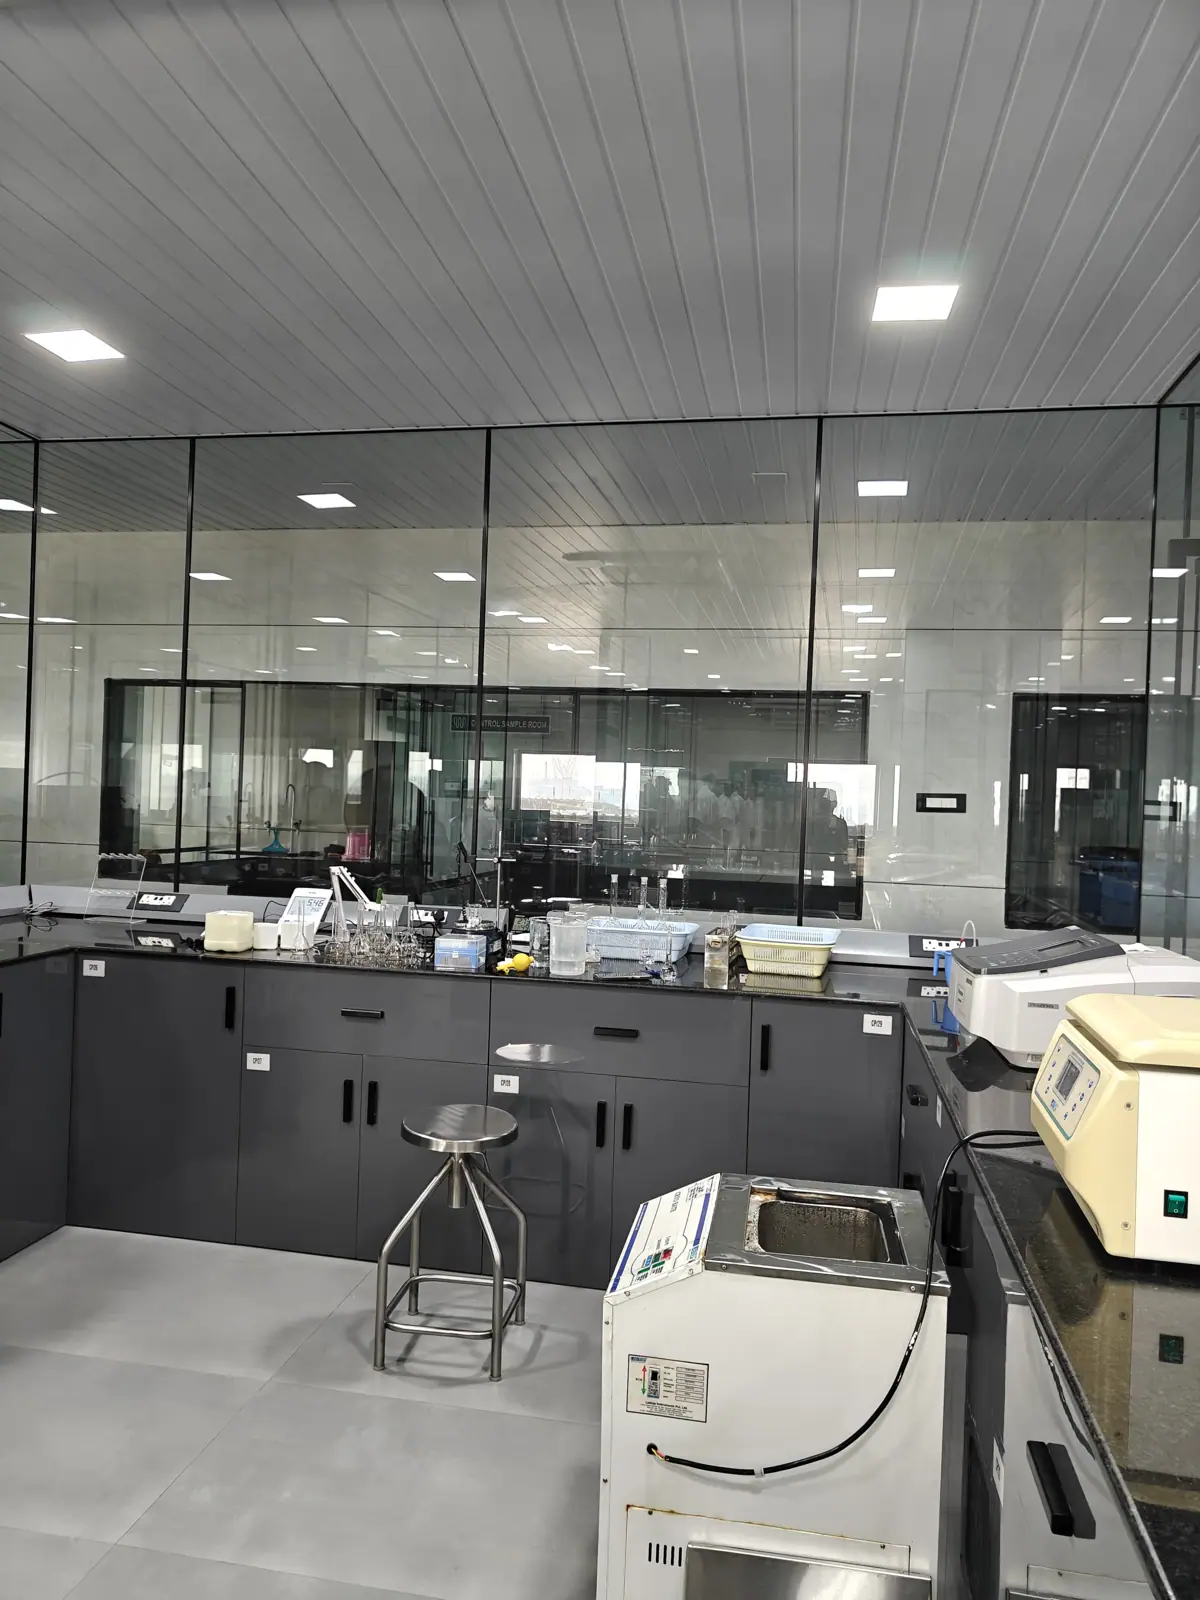
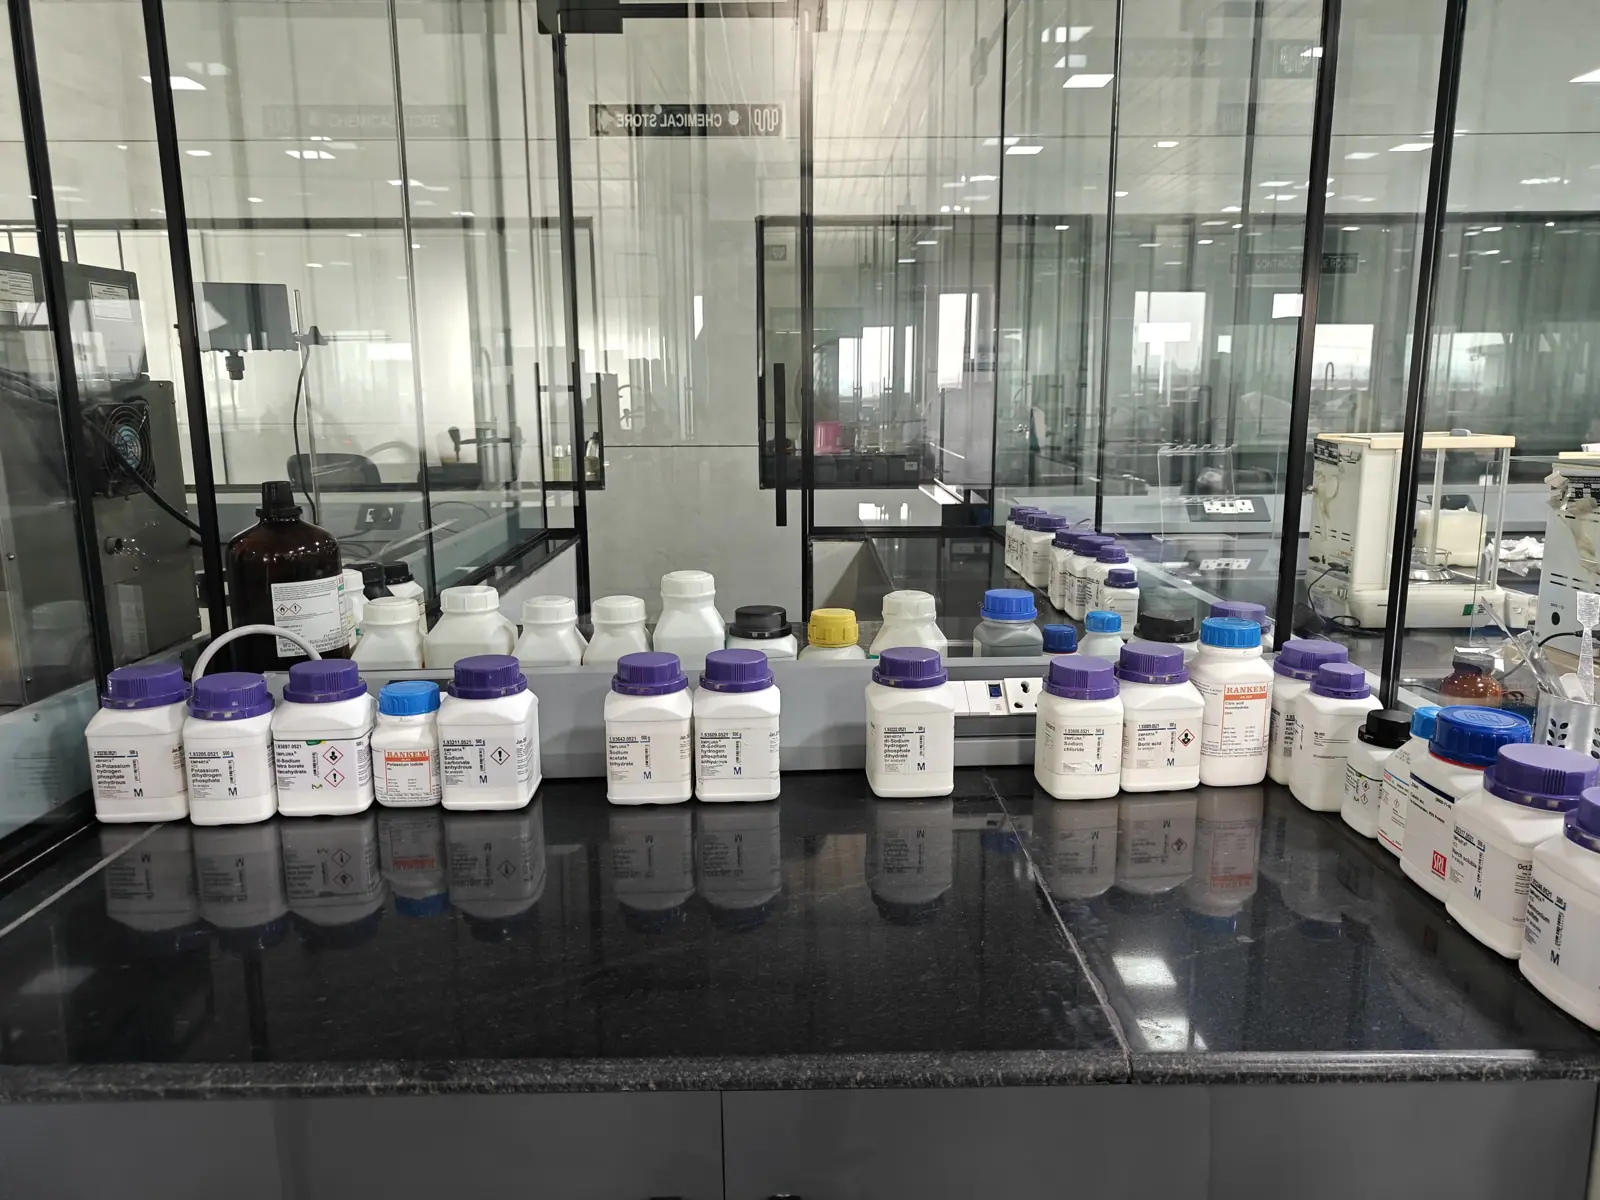
Raw materials are checked before they are used.
Every incoming raw material is sampled and tested by our own quality control laboratories before it is released to production — the first gate a batch passes.
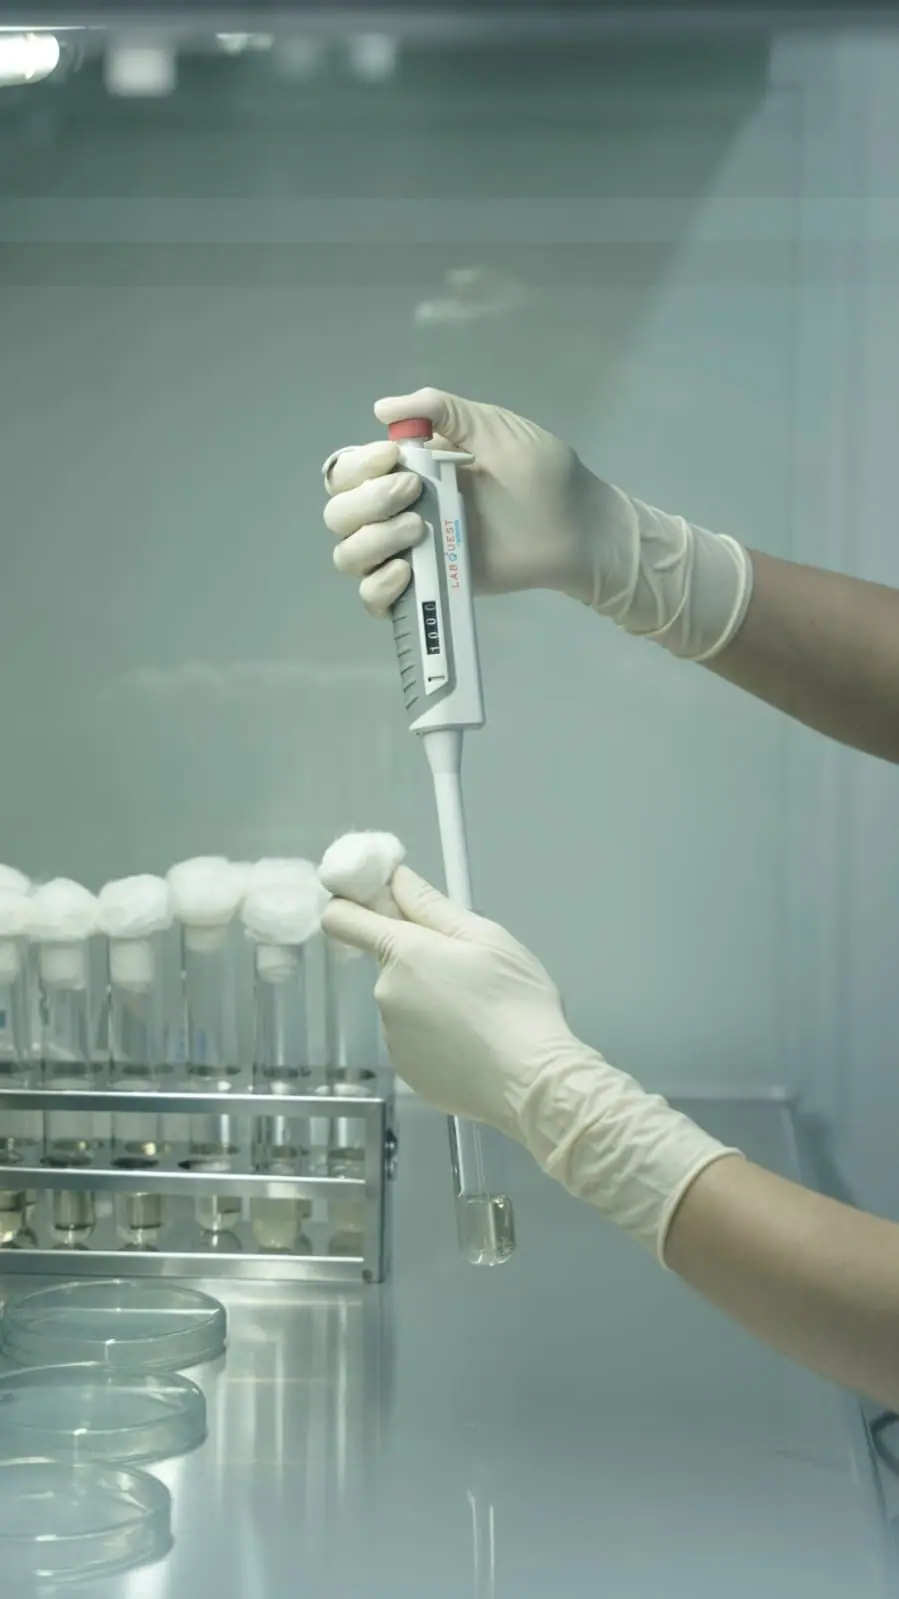
- Microbiological testing of raw materials for microbial quality and purity
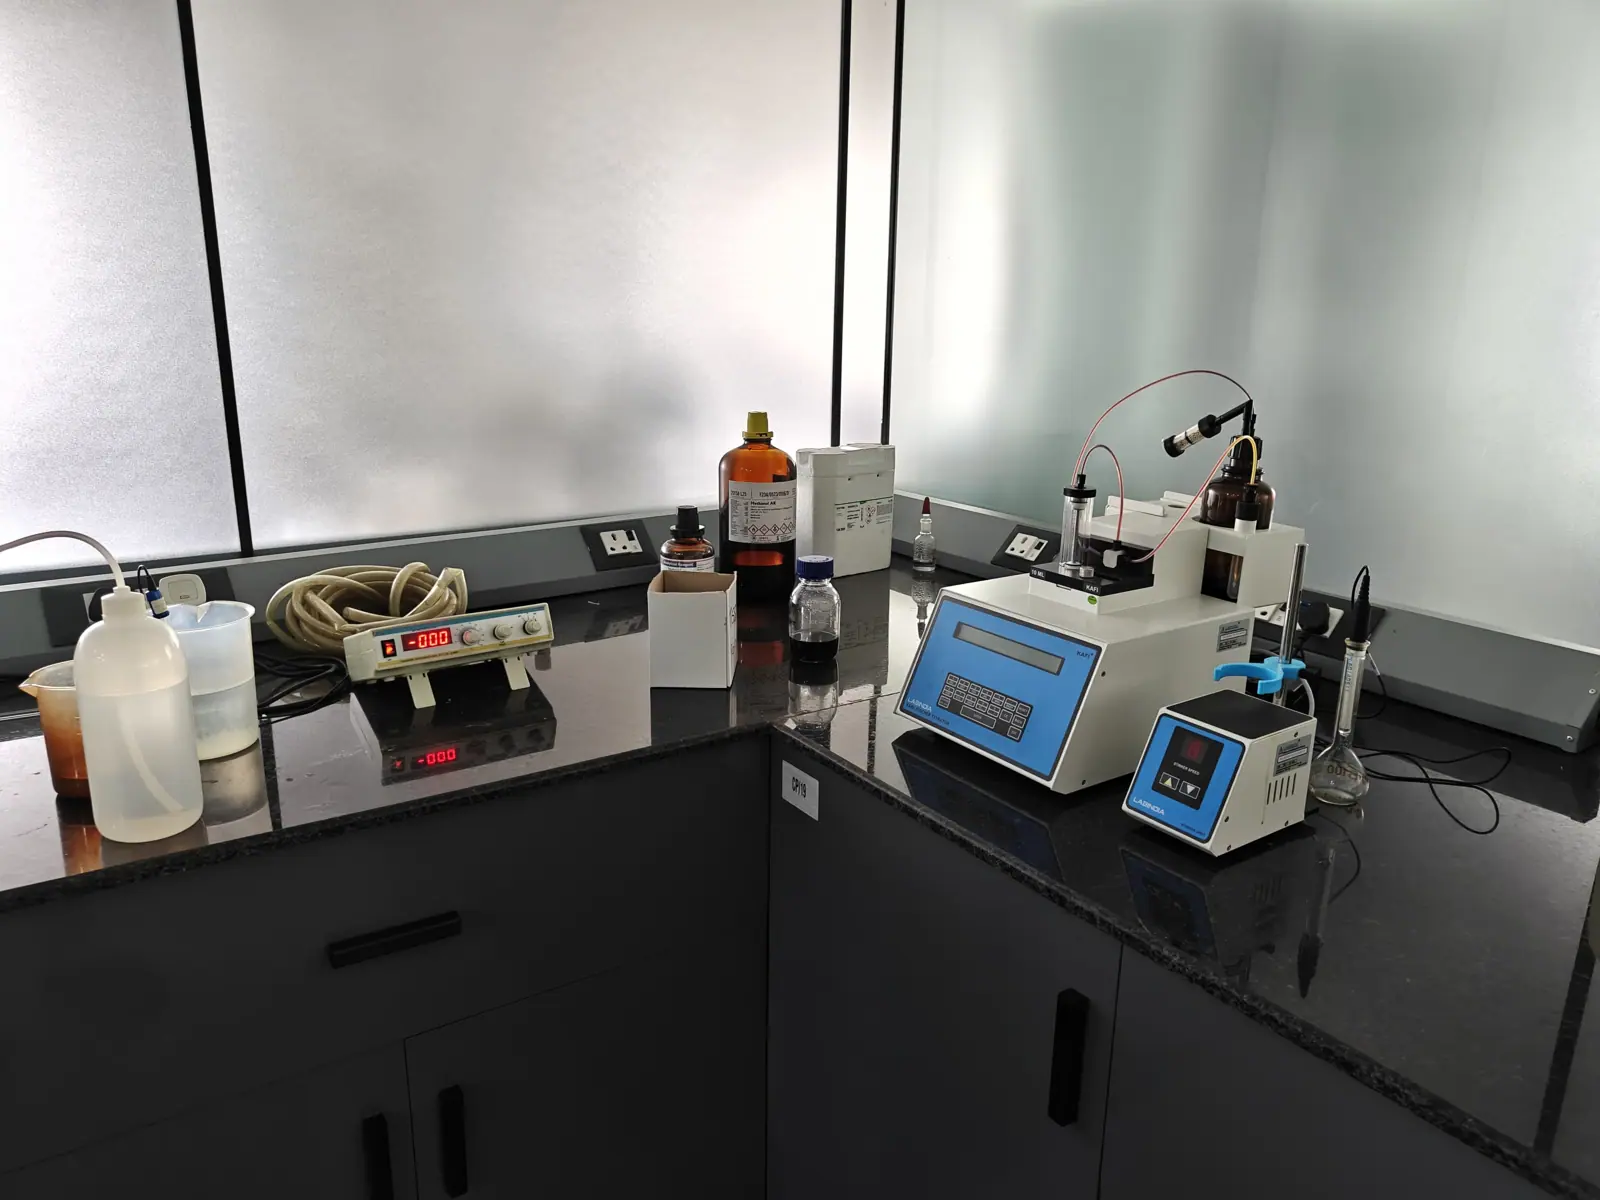
- Chemical checks against the material specification
- Only released materials move on to R&D or production
The process is designed and scaled in our own R&D labs.
Two separate research laboratories develop and optimise processes before anything reaches the production floor — one for fermentation, one for API-related work.
- Fermentation process development, optimisation and scale-up studies
- API-related research, process development and analytical support
- Custom blends formulated to your application, dose and format
Enzymes and probiotics are made in separate units.
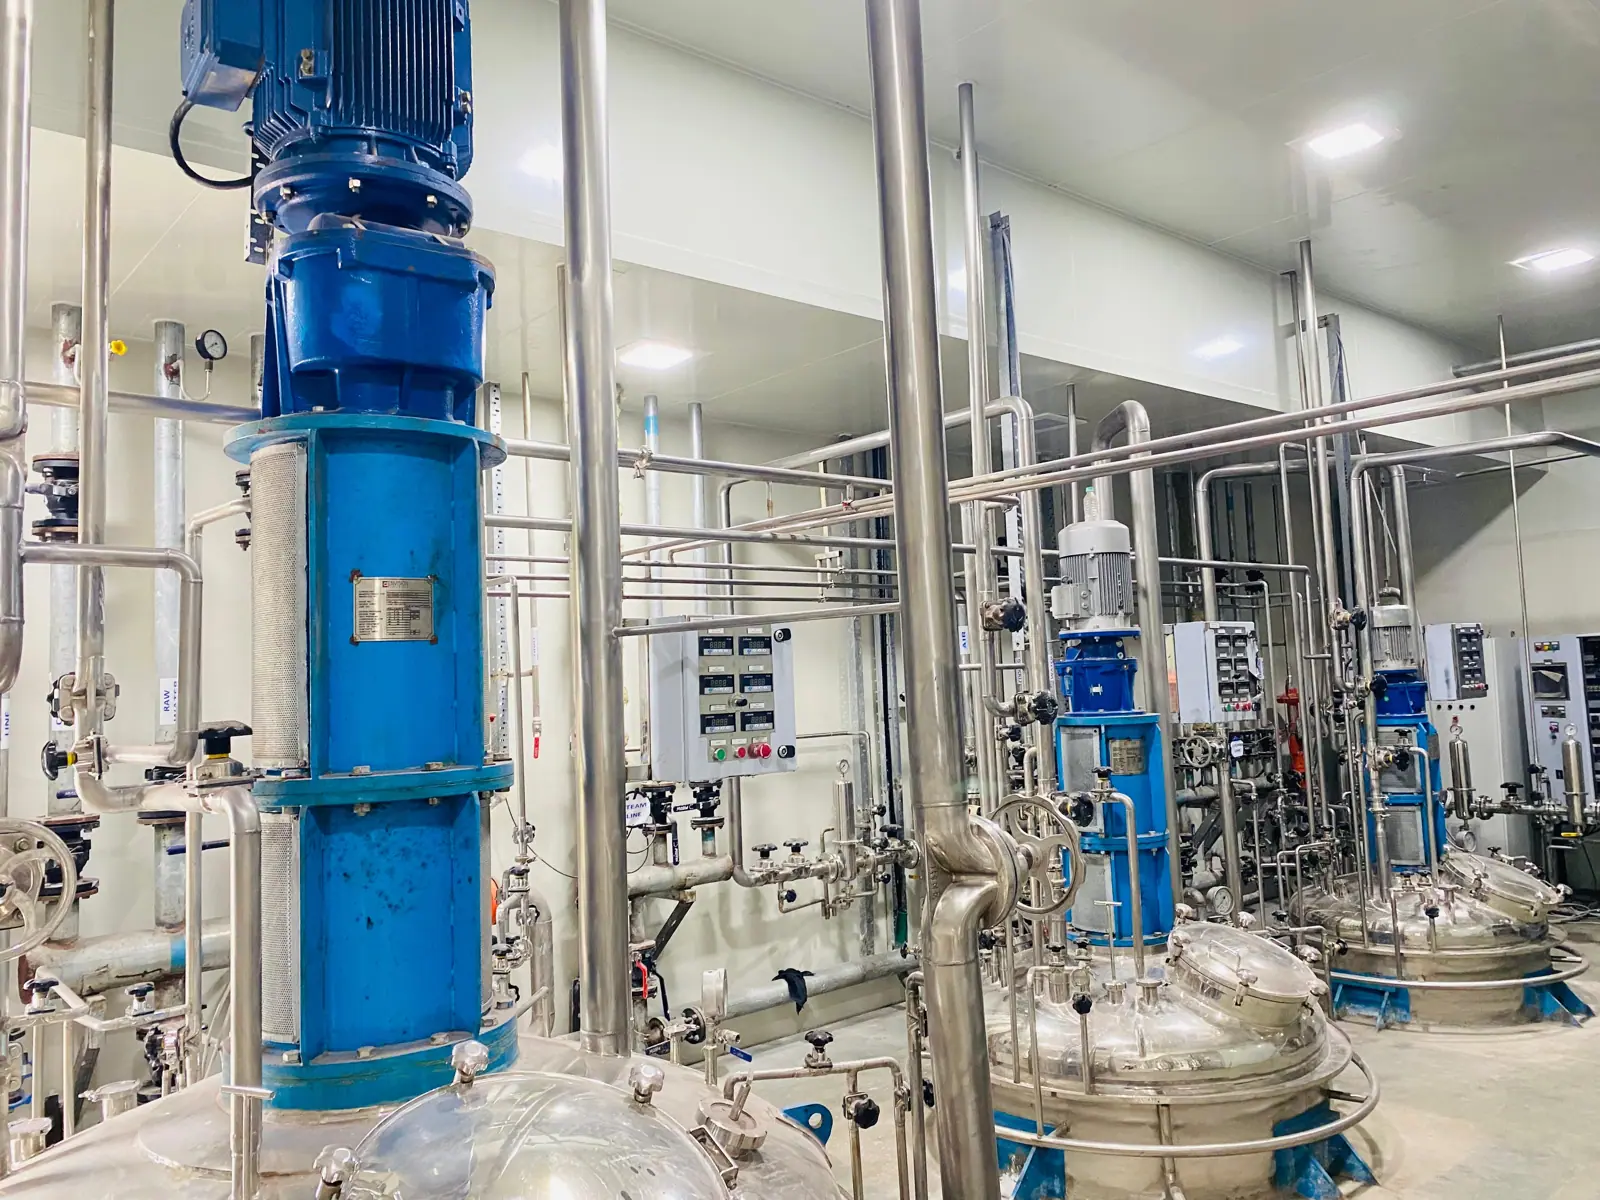
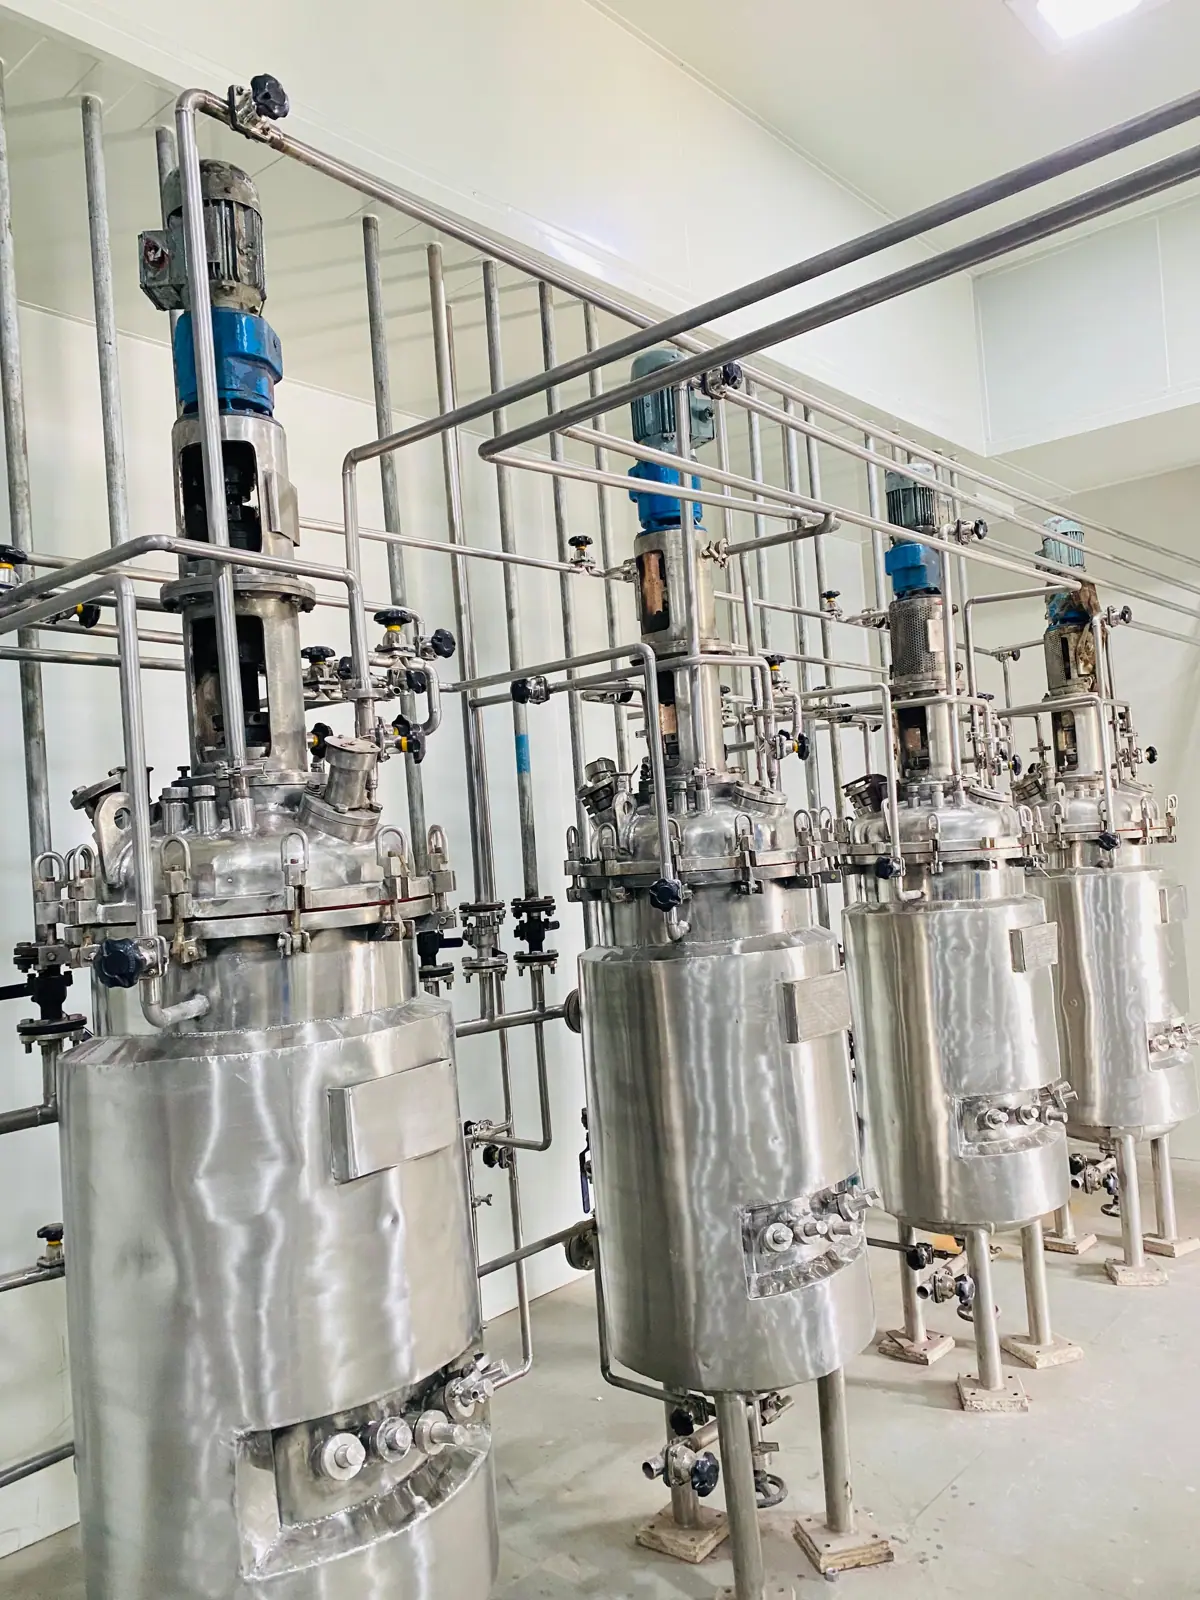
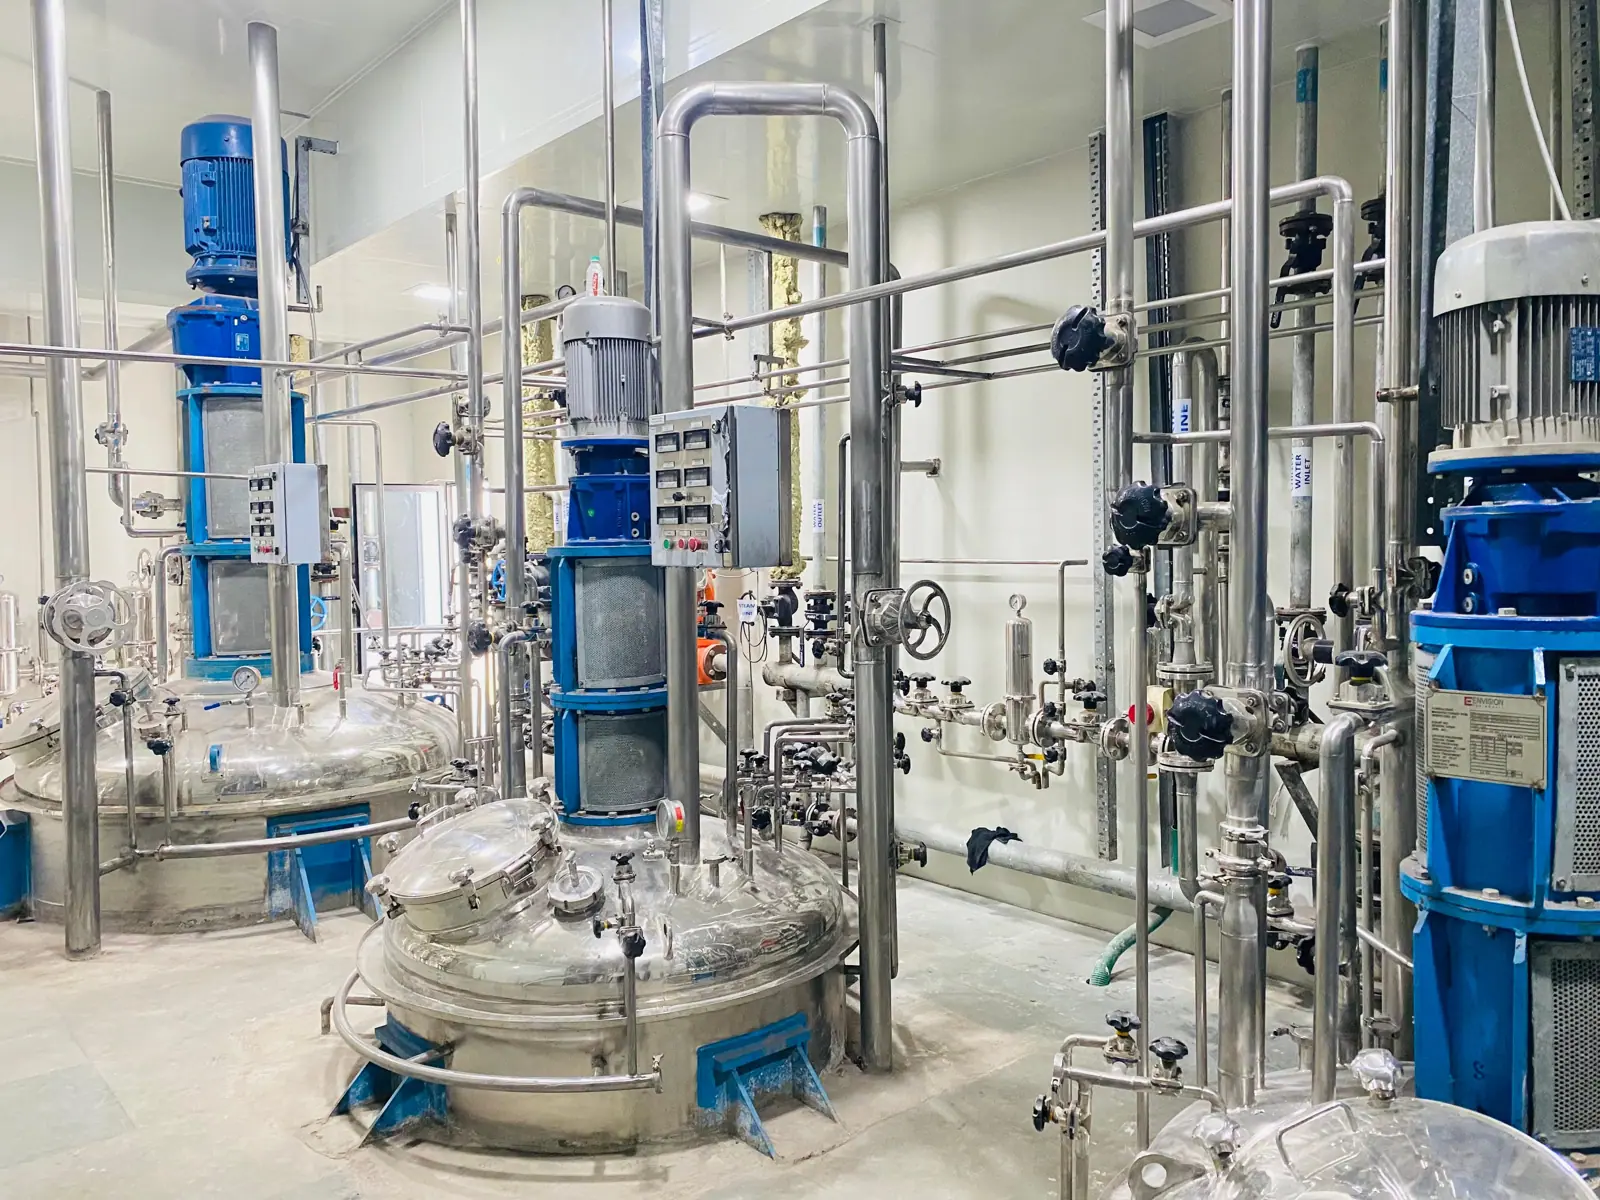
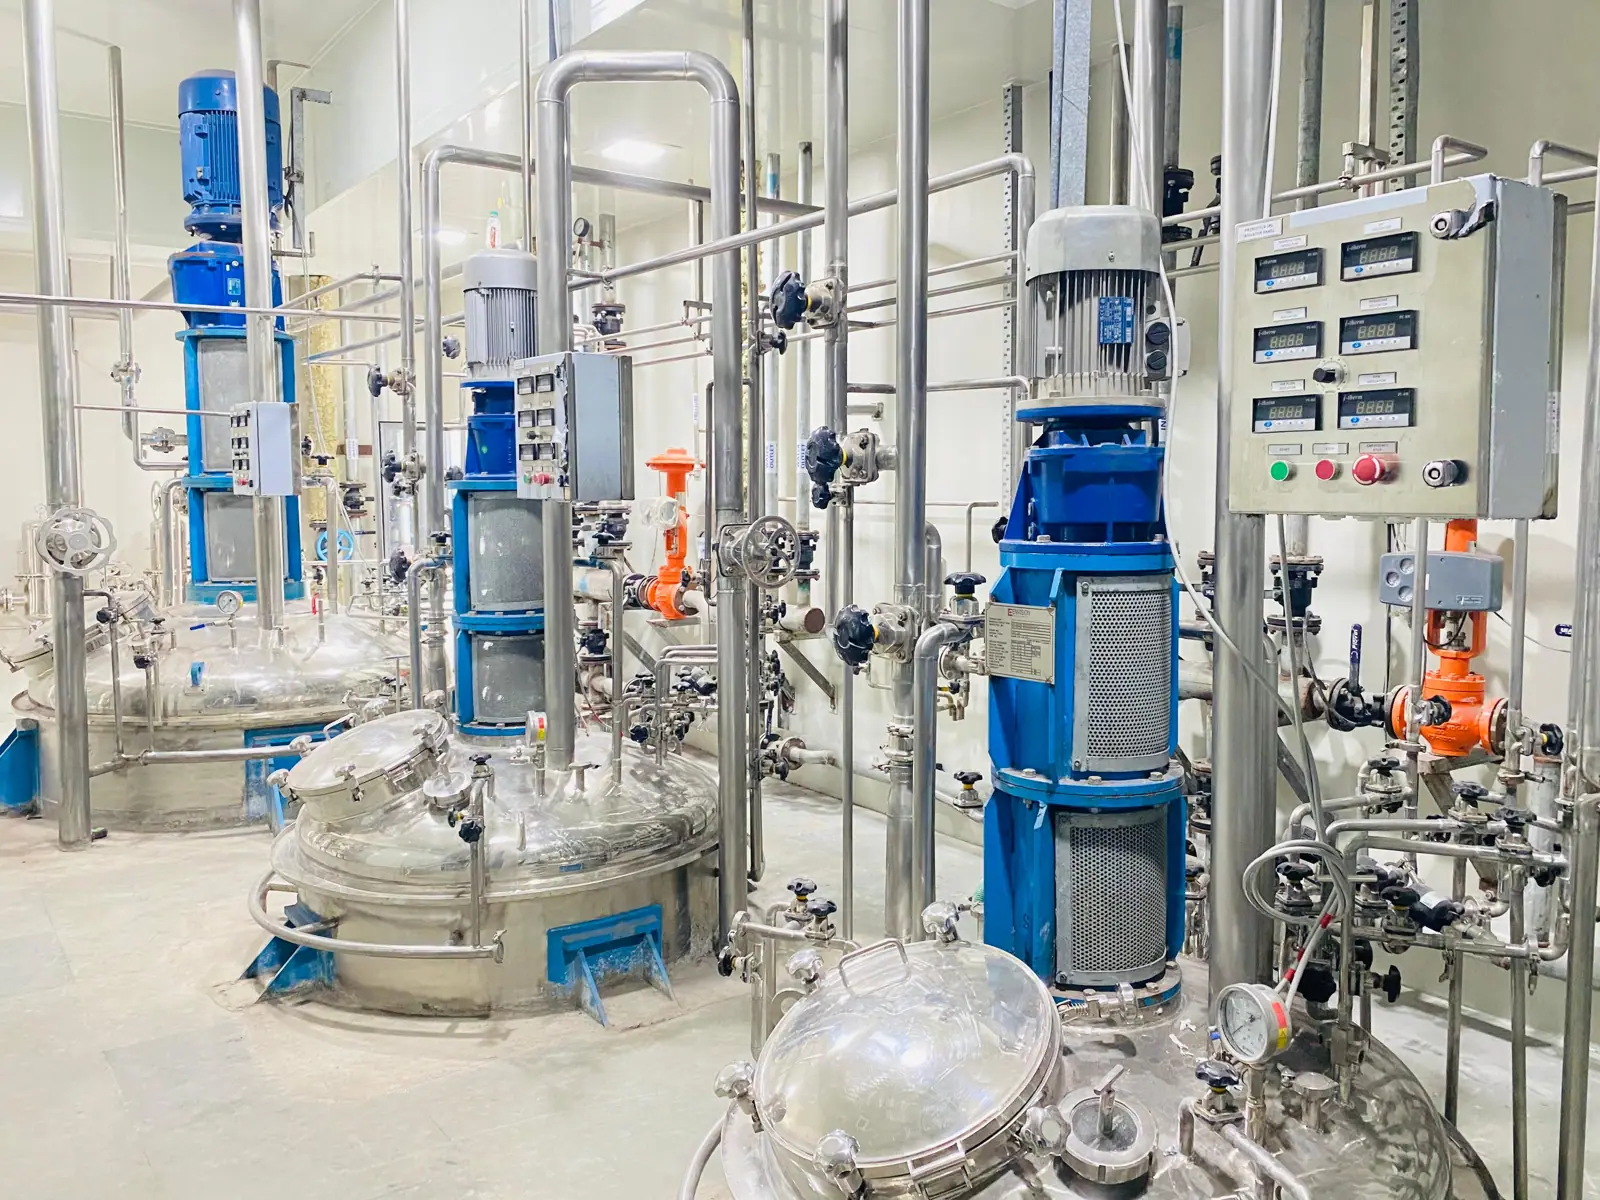
Production runs in two dedicated fermentation facilities: one for enzymes and a separate one for probiotics, so each process is controlled on its own.
- Enzyme fermentation unit focused on consistent, reliable production
- Separate probiotic fermentation unit for controlled production of strains
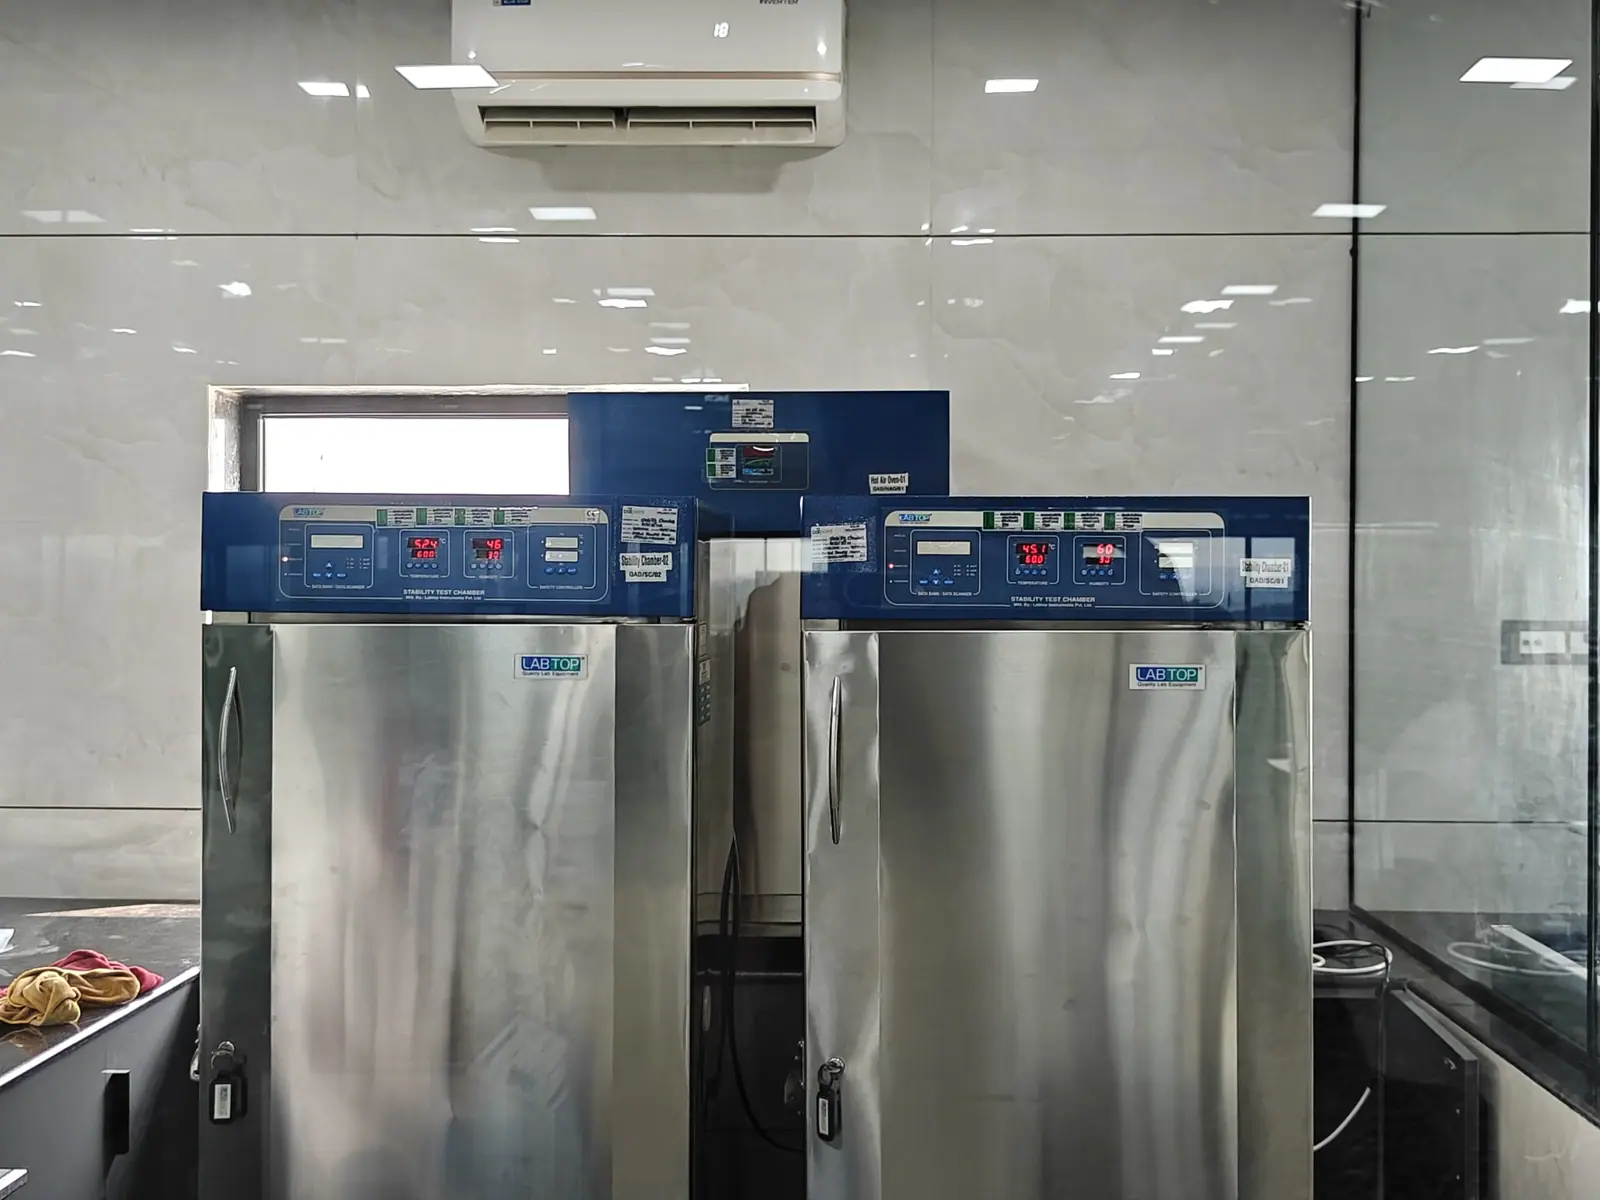
- Stainless-steel fermenters with in-process monitoring
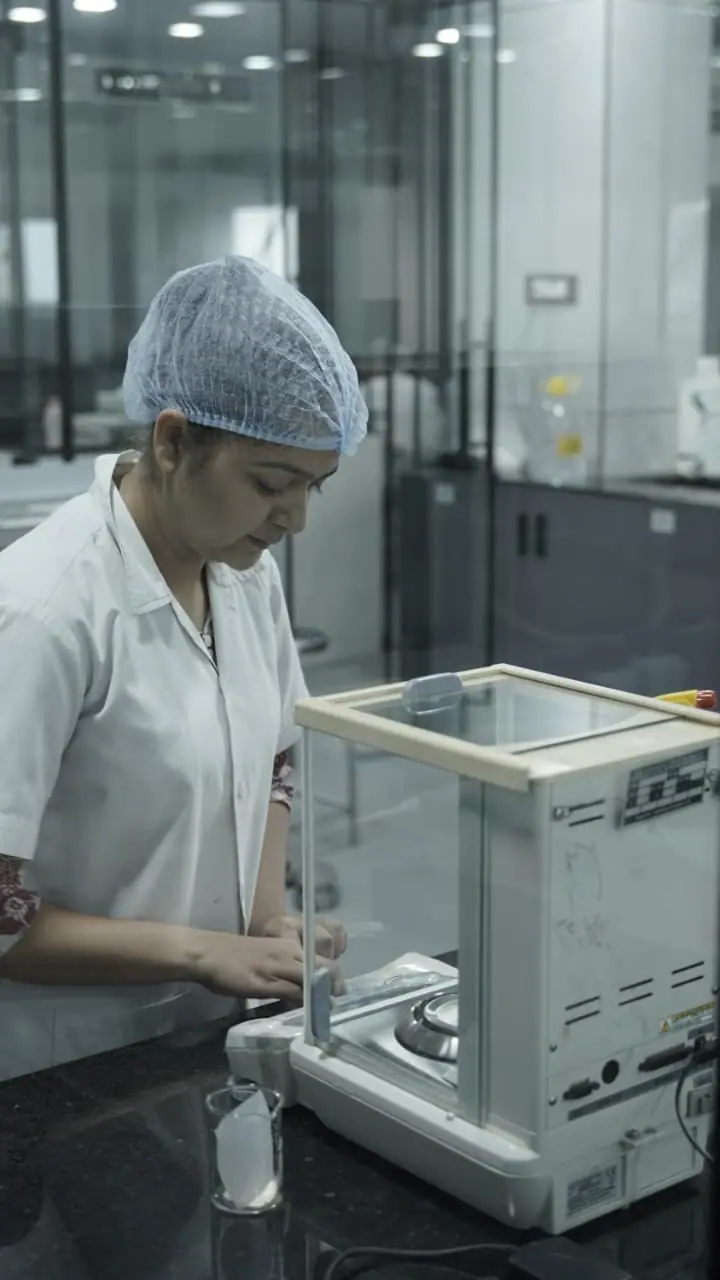
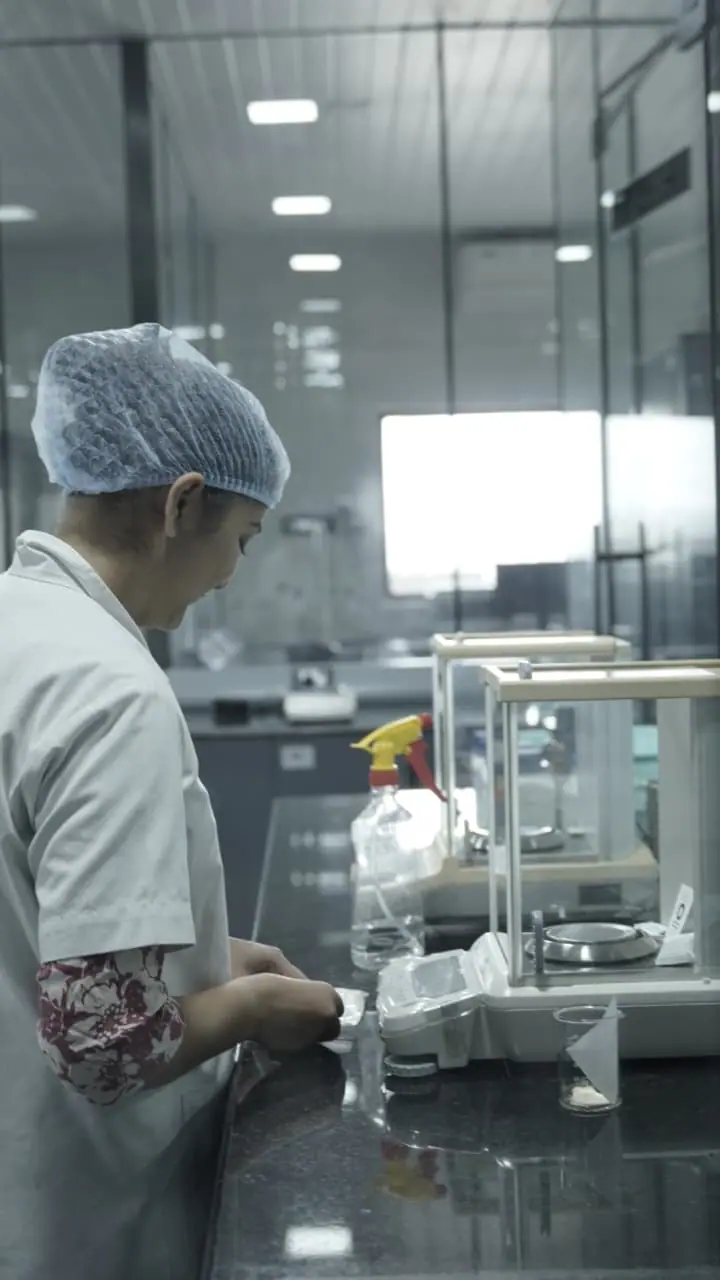
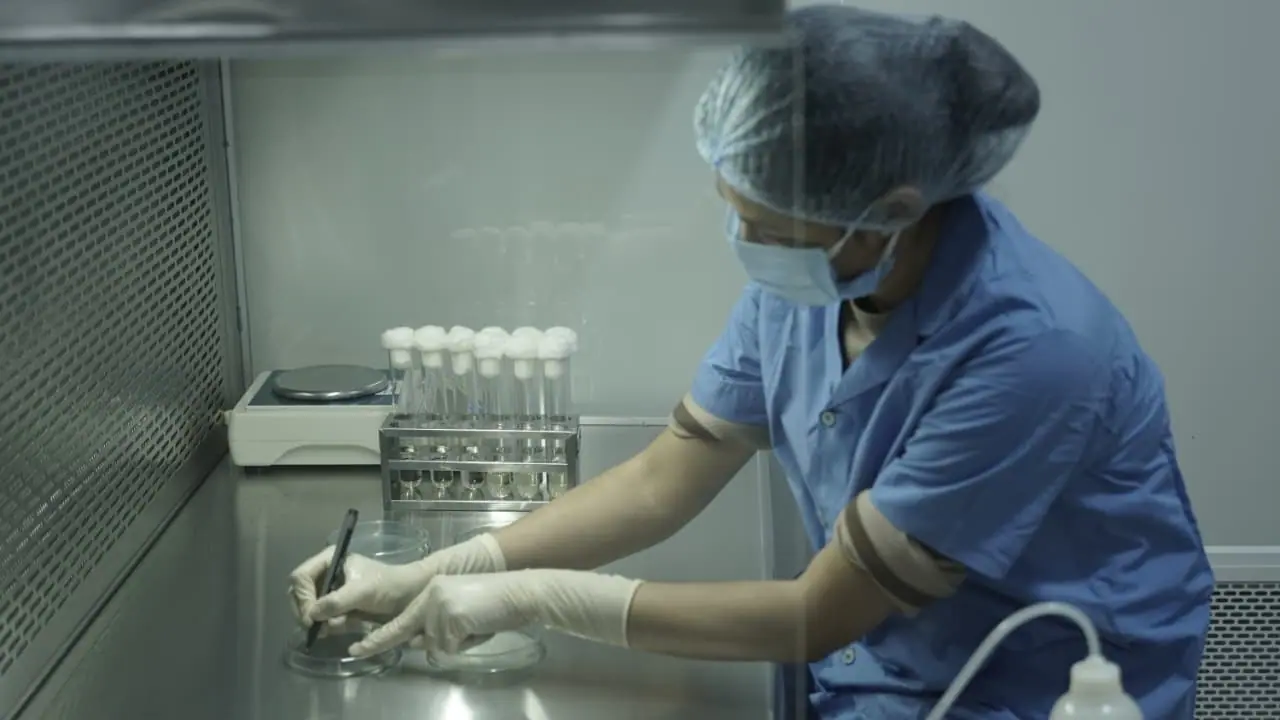
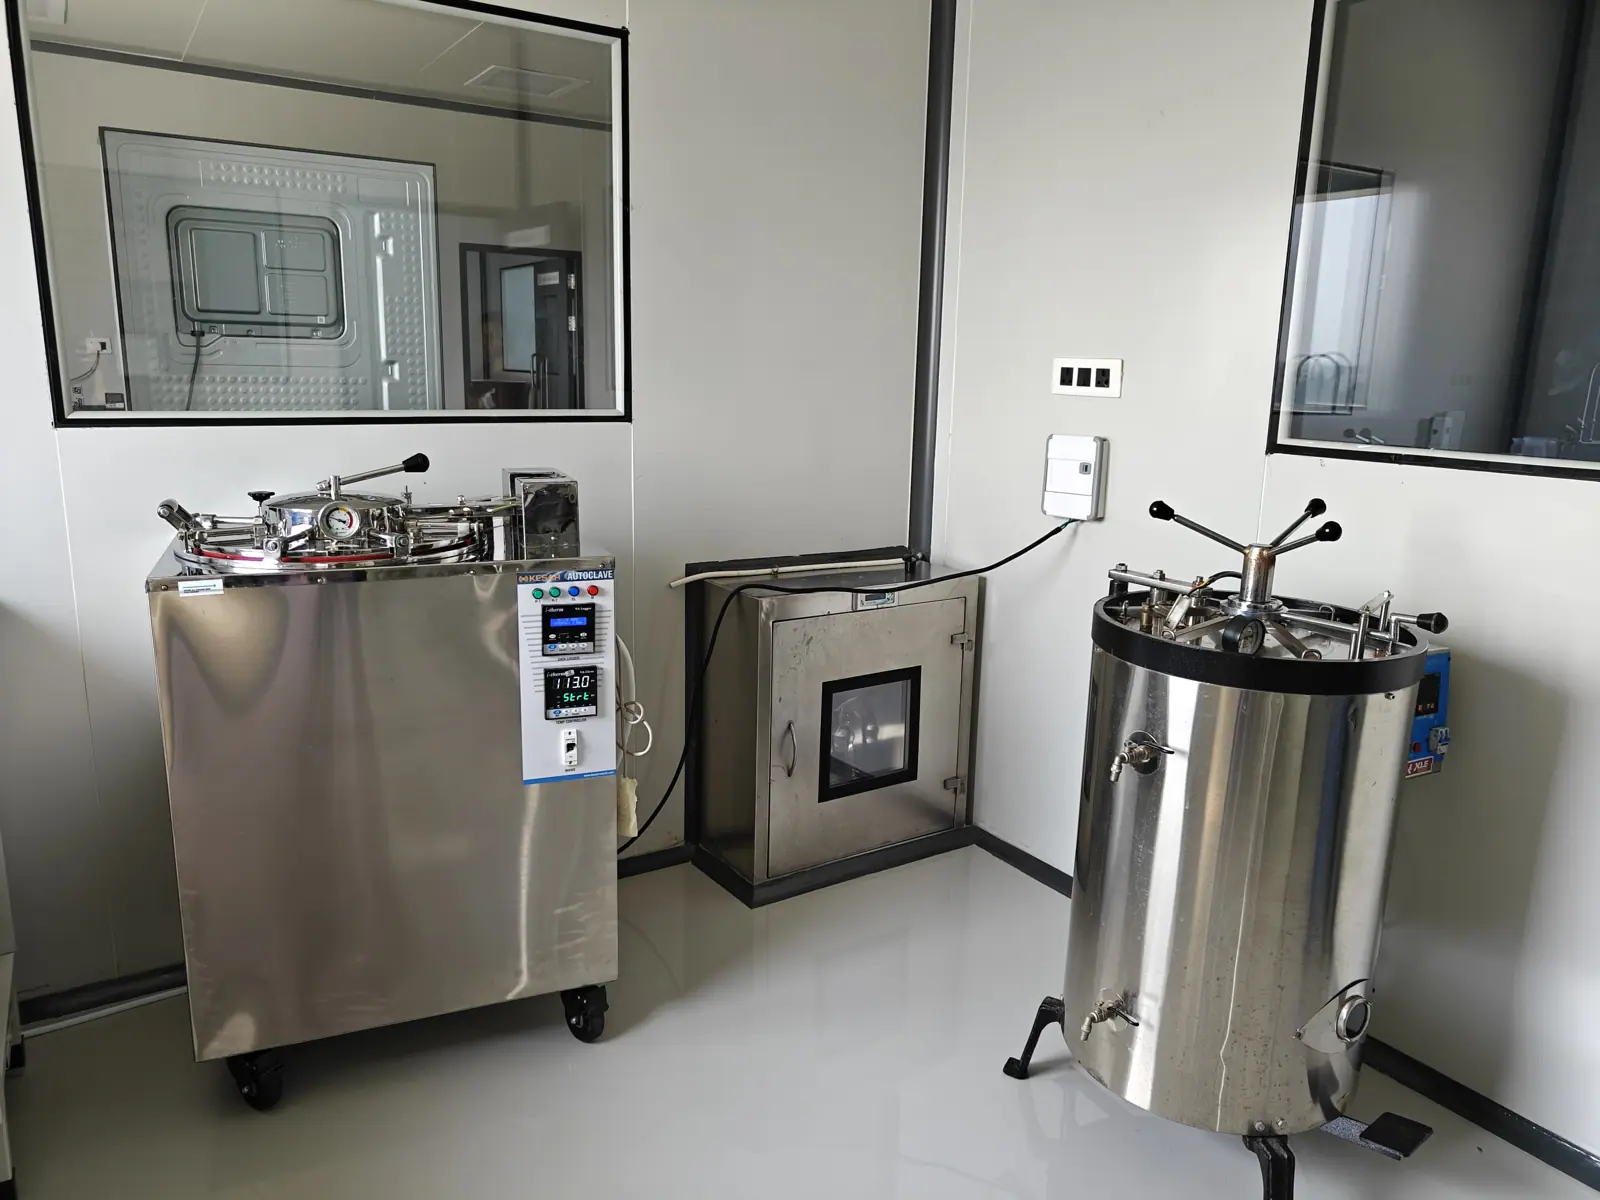
Every batch is tested by two QC laboratories.
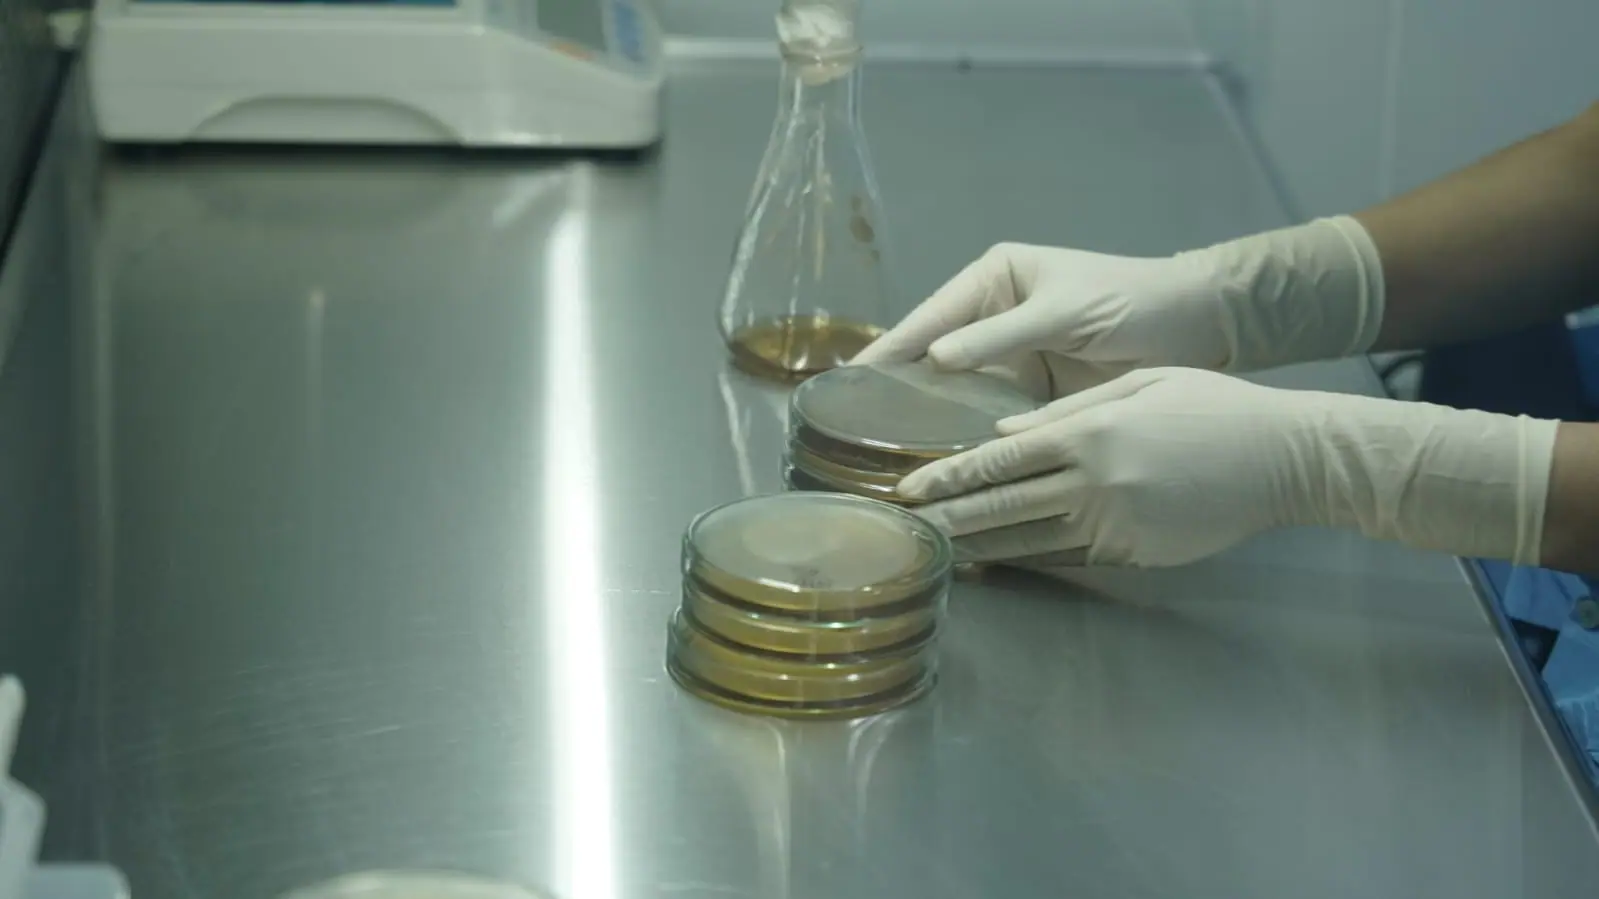
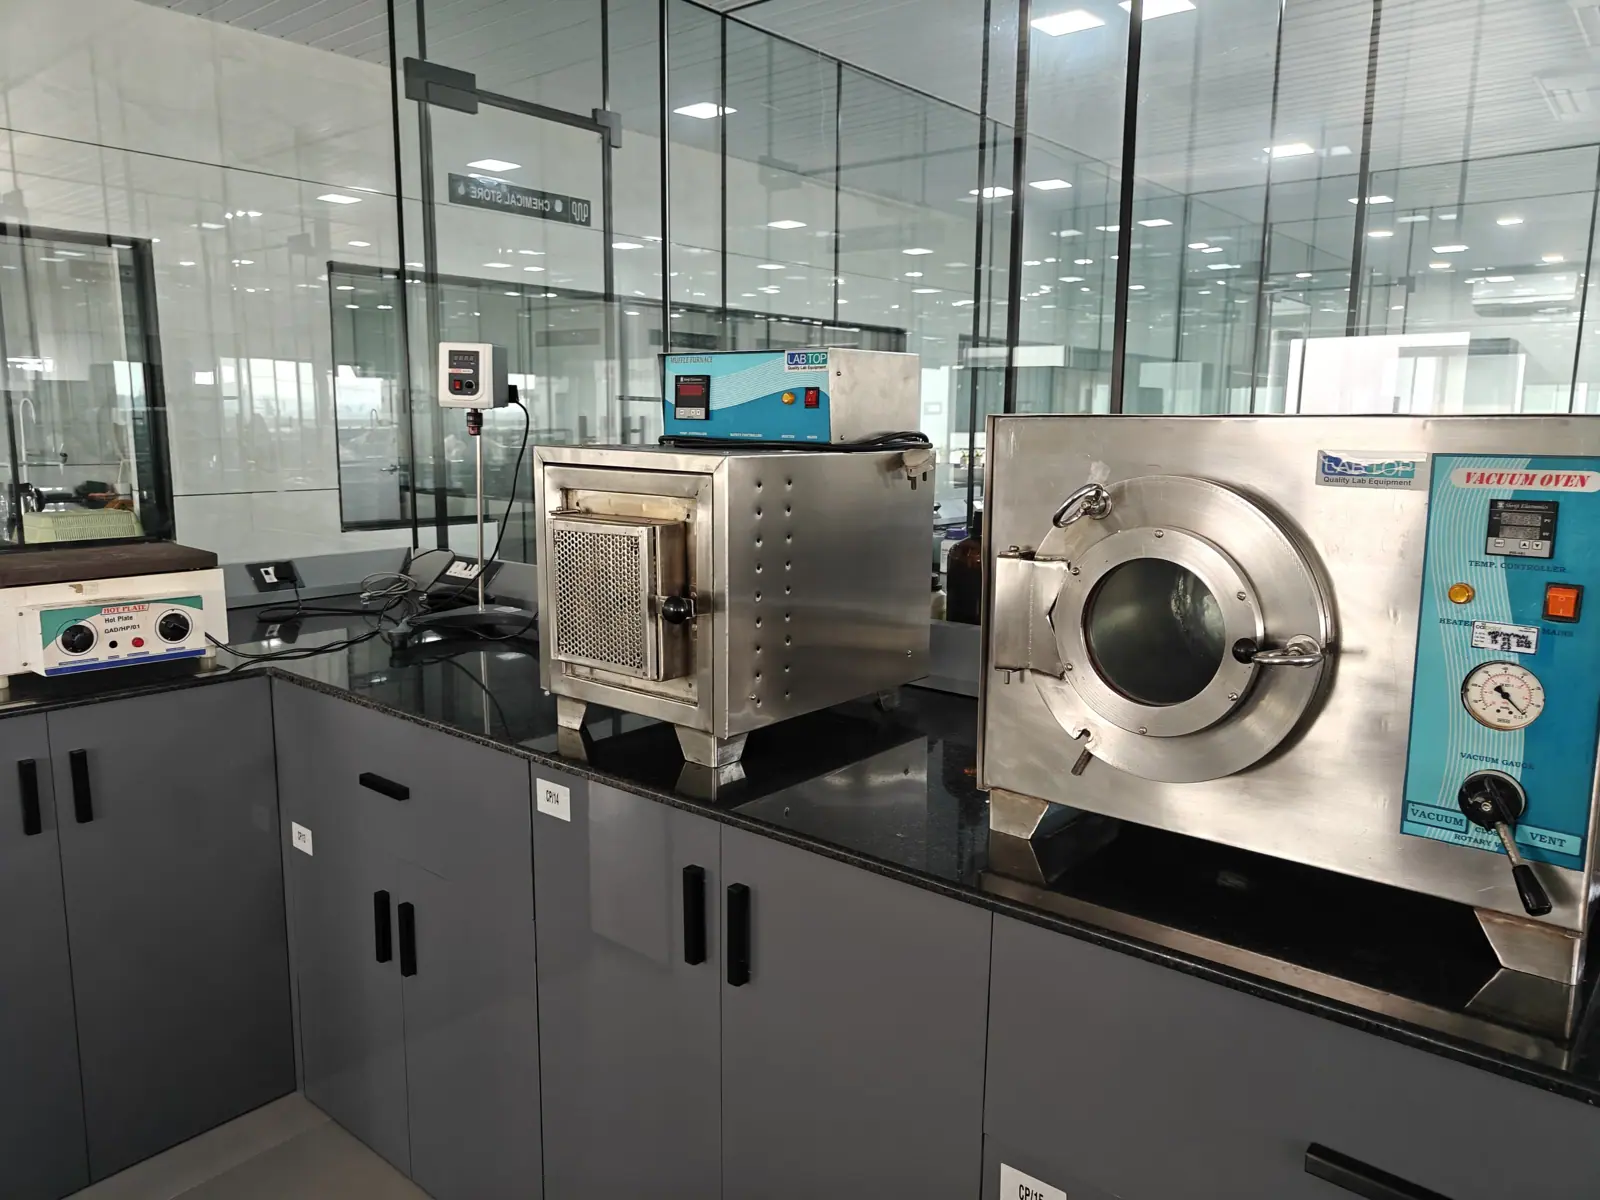
Finished batches are tested independently of production — chemically for activity and potency, and microbiologically for purity and microbial limits.
- Chemical QC: product specification, enzyme activity, potency and critical parameters
- Microbiological QC: microbial quality, purity and related parameters
- Results recorded on a certificate of analysis for the batch
QA reviews the records and releases the batch.
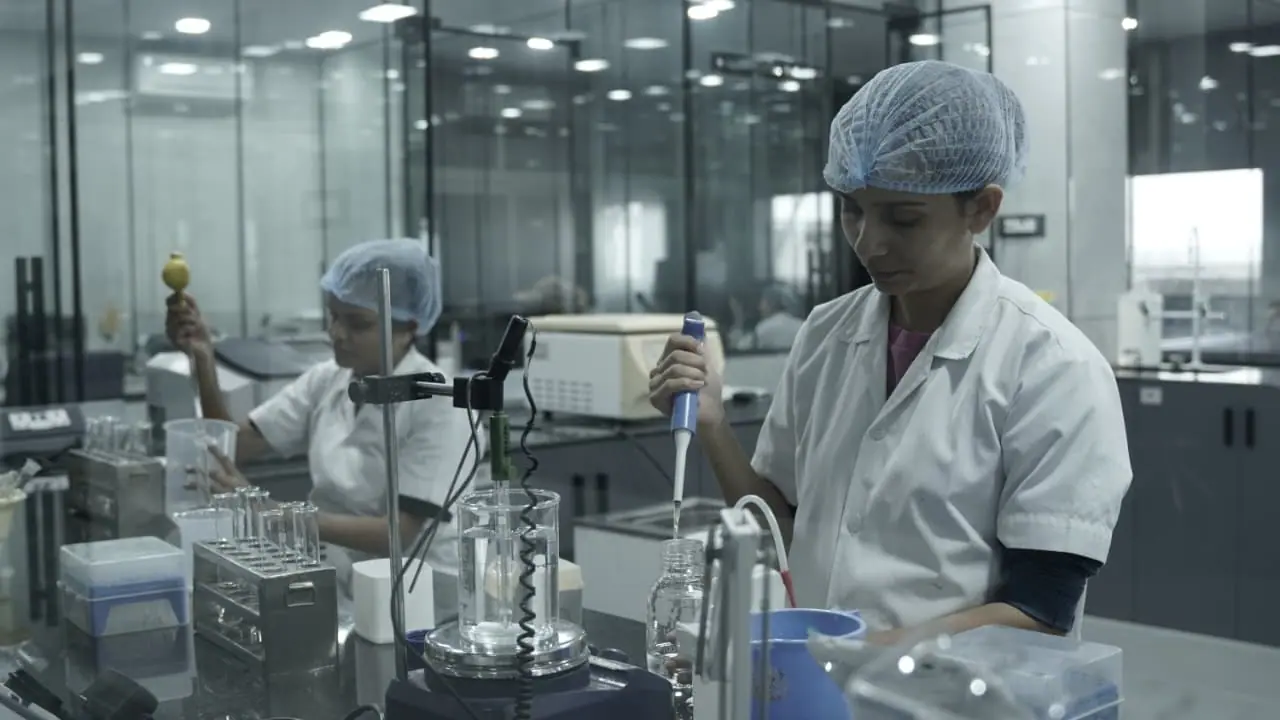
Our Quality Assurance department runs the quality system around all of this — documentation, process compliance and the review that releases a batch for dispatch.
- Batch documentation and process-compliance review
- Release only after QC results meet the specification
- Quality systems certified to ISO 9001:2015, FSSC 22000 and GMP
Packed, documented and shipped to you.
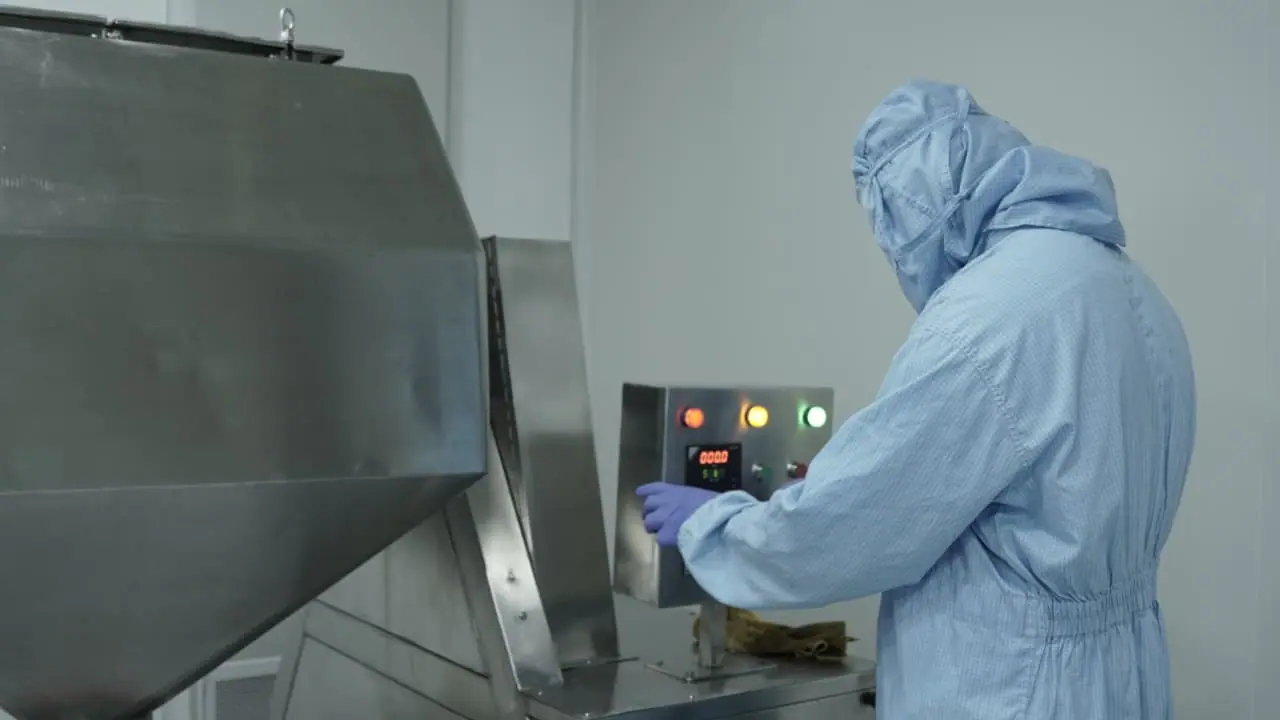
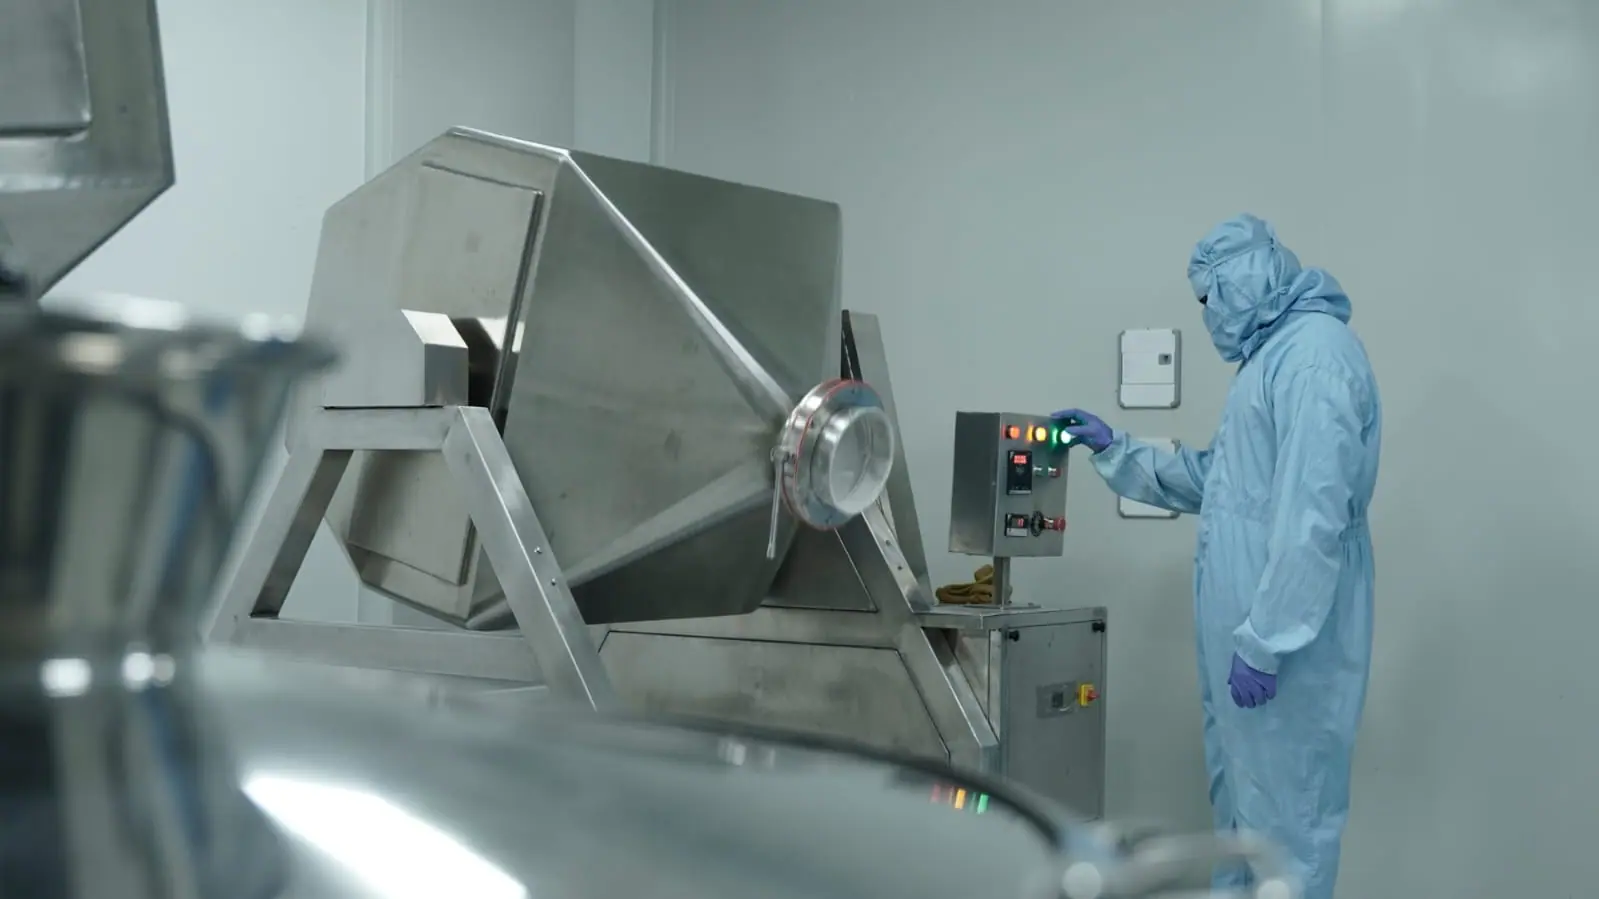
Released product is packed in a clean area and shipped with its documents — to customers in India and 20 export countries.
- 25 / 50 kg HDPE drums or retail pouches; custom packing on request
- Technical data sheet and batch certificate of analysis
- Commercial invoice and packing list with every consignment
What arrives with every order.
Let’s build your next formulation.
Tell us about your application — we’ll recommend the right enzyme, share technical data and send samples.